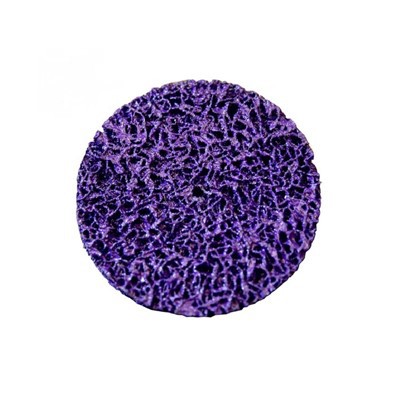
Non-woven Abrasives Production Process
1. Melt the polymer slices of each component through a screw extruder to form a fiber melt;
The components include by mass parts: 60-90 parts of polyamide fiber, 20-30 parts of carbon fiber (PAN), 0.5-1.0 part of metal fiber;

2. Spray the fiber melt into fiber form through the spinneret hole, and form extremely fine short fibers under the blowing of 13000m/min high-speed hot air;

3. Short fiber wear resistance spray treatment.
The abrasion resistance treatment includes: in parts by mass, 30-50 pieces of epoxy resin, 6-15 parts of curing agent, 20-45 slices of abrasive, 3-4 parts of the toughening agent, silane even 1-3 parts of the joint agent, after mixing evenly, spray the short fiber through the spray equipment.

4. The short fibers are adsorbed on the web-forming curtain, and the fibers are condensed into industrial scouring pads.
Manufacturing equipment for industrial scouring pads, including melt-blown equipment, the melt-blown equipment includes a suction port, a spring buckle, a fuselage, a feed port, a spray device, and a spray inlet. The fuselage is connected to one end of the feed port, The spring buckle is located at the edge of the other end of the feed port, and the air suction port is surrounded by the outer layer of the feed port. It forms a suction cavity with the feed port, and a meltblown die is set inside the fuselage. The inside of the fuselage of the spray equipment is connected to the meltblown die.